
Powder Coatings for Power Equipment and Energy Storage: Corrosion Protection, Durability and Reliable Manufacturing
1. Why Surface Protection Matters in Modern Power Equipment
The rapid development of electrical infrastructure, renewable energy and energy storage is creating new requirements for metal surface protection.
From electrical distribution cabinets and transformer enclosures to EV charging stations and battery energy storage systems, metal components are increasingly exposed to demanding operating environments.
For equipment manufacturers, a coating must do more than provide an attractive appearance. It must help protect the substrate, maintain consistent surface quality and support reliable industrial production.
Outdoor electrical cabinets may experience humidity, temperature fluctuations, rain and industrial pollution. Equipment installed near coastal areas may also face salt-laden air.
These conditions make powder coating selection an important part of equipment design and manufacturing.
A suitable powder coating system can provide decorative appearance, mechanical durability and corrosion protection while supporting efficient factory application.
However, not every powder coating is appropriate for every electrical application. The coating must be selected according to the substrate, operating environment and technical requirements.
2. Different Electrical Applications Require Different Coating Systems
Electrical equipment covers a wide range of products, and each application presents different coating challenges.
Electrical Distribution Cabinets
Distribution cabinets and switchgear enclosures commonly use steel sheet components that require consistent appearance and reliable surface protection.
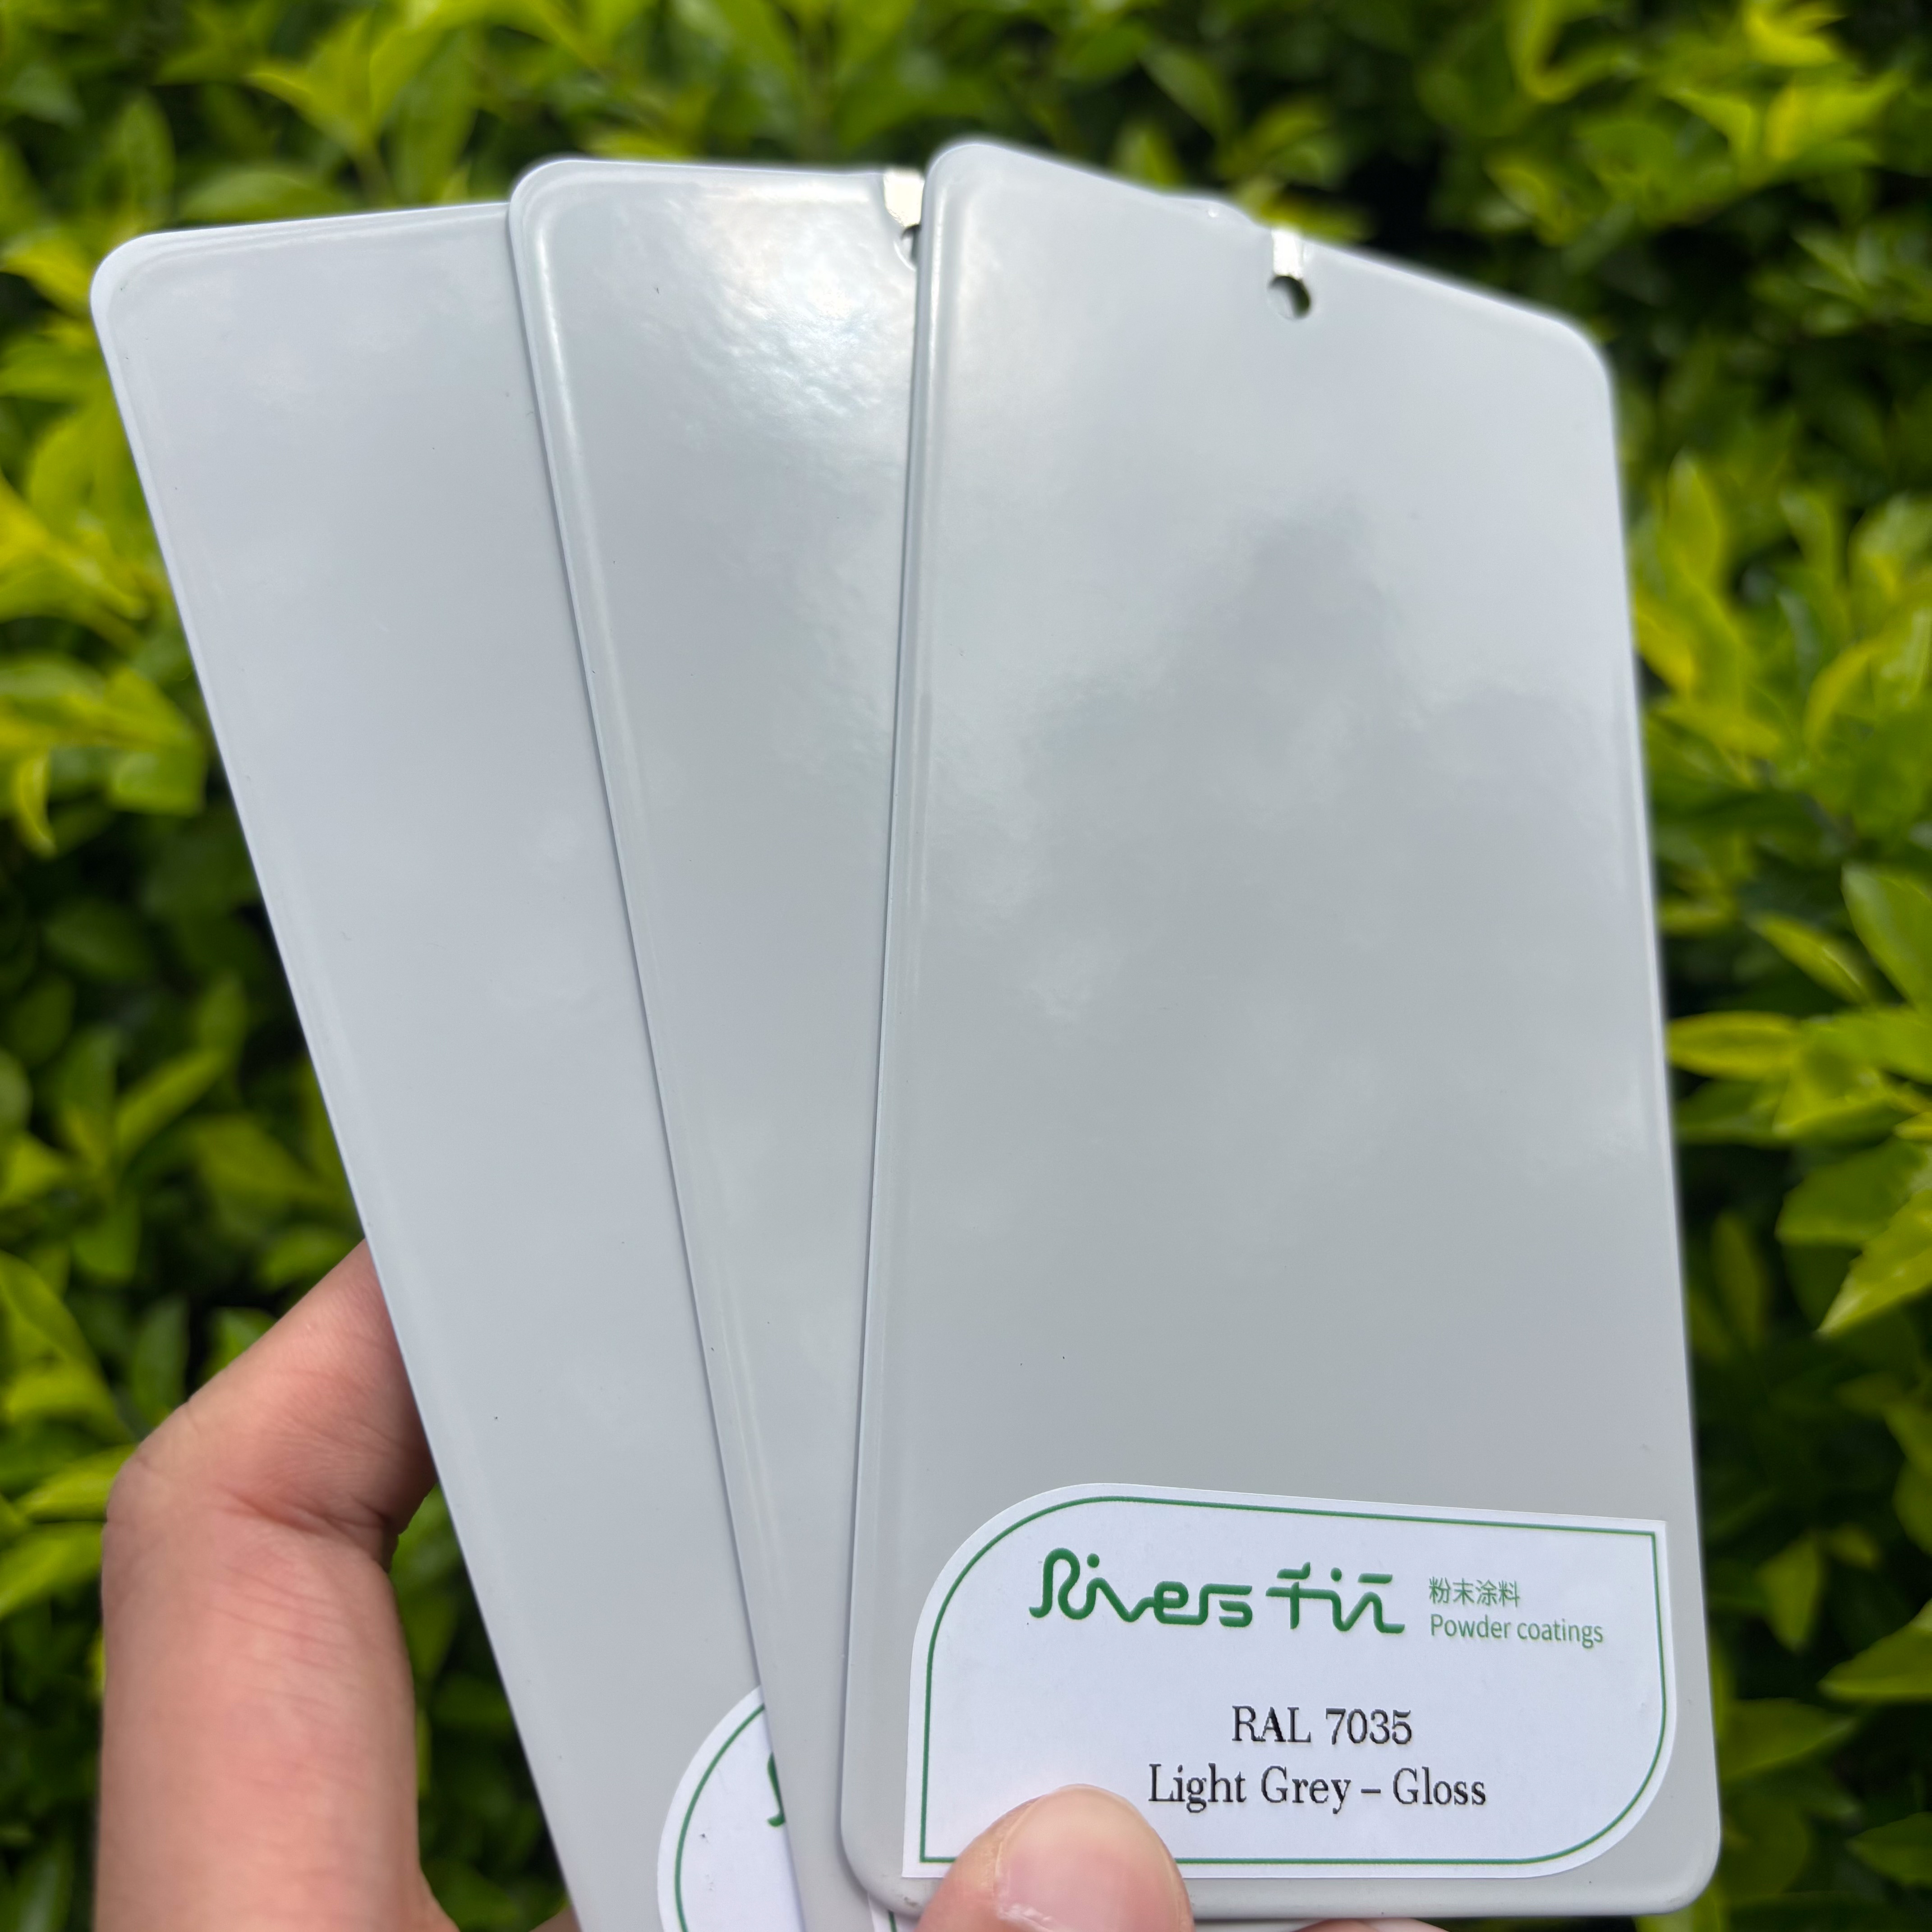
Popular finishes include light grey, textured grey and other neutral industrial colors.
RAL 7035 and RAL 7032 are widely recognized color references for electrical equipment, although individual manufacturers may specify different shades and surface textures.
For indoor installations, decorative performance and mechanical durability may be primary considerations.
Outdoor installations require additional attention to weather resistance and corrosion protection.
EV Charging Stations
EV charging stations combine electrical functionality with visible exterior design.
Their housings may be installed in parking areas, commercial buildings, residential developments and public infrastructure.
A suitable coating must balance exterior appearance with resistance to environmental exposure.
For manufacturers, consistent color and gloss are also important because charging equipment often forms part of a recognizable product family.
Battery Energy Storage Cabinets
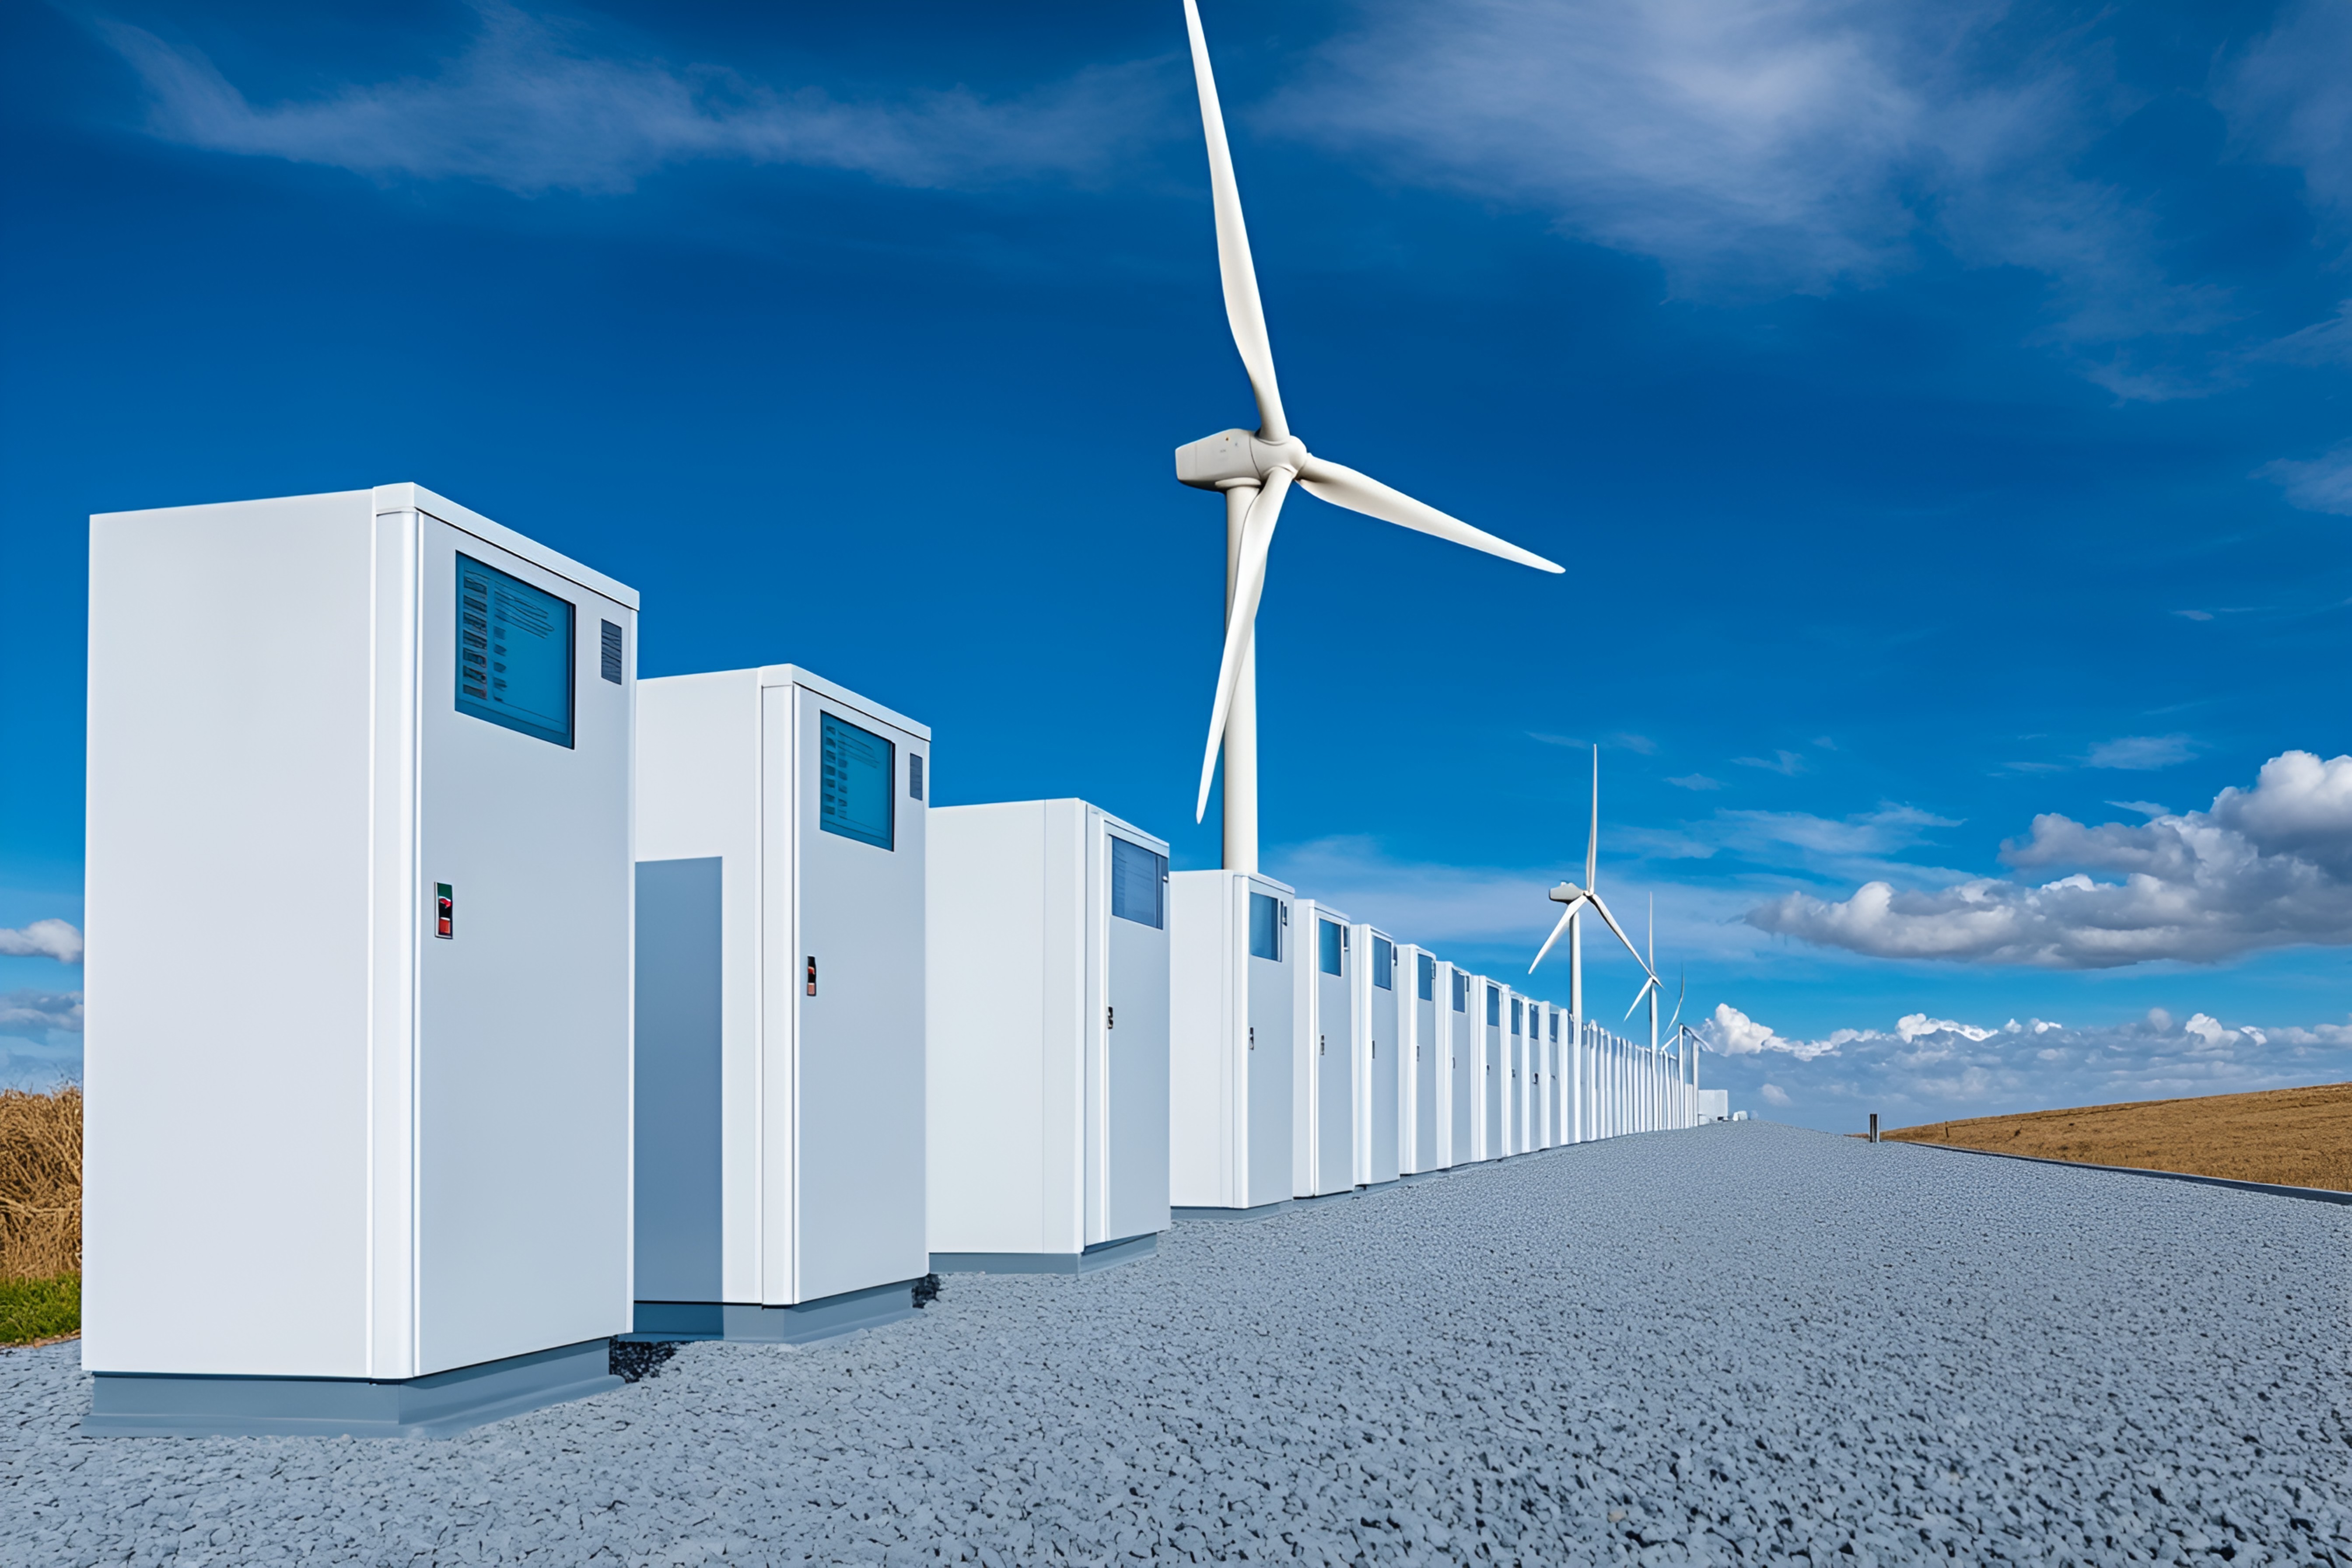
Battery energy storage systems may operate in outdoor industrial environments for extended periods.
Their metal enclosures require appropriate protection against moisture, corrosion and mechanical damage.
Coating selection should consider the installation environment, enclosure construction, substrate preparation and expected service conditions.
Where electrical insulation or fire-performance requirements apply, these must be evaluated separately using the relevant product specifications and testing methods.
3. Understanding Corrosion Protection Requirements
Corrosion protection is one of the most important considerations for outdoor electrical equipment.
International projects frequently refer to ISO 12944 when defining environmental corrosivity and protective coating requirements for steel structures.
For example, C3 and C4 environments represent different levels of atmospheric corrosivity.
A coating system intended for a moderately corrosive environment may not be suitable for more aggressive industrial or coastal exposure.
The required protection depends on several factors:
Steel substrate condition and surface preparation.
Pretreatment method and coating-system structure.
Primer and topcoat selection.
Total dry film thickness.
Installation environment and expected durability.
For more demanding applications, a two-layer powder coating system may be considered.
An epoxy powder primer can contribute to corrosion protection and adhesion, while a suitable weather-resistant polyester topcoat provides exterior appearance and weatherability.
However, an ISO 12944 corrosivity category does not automatically certify a particular powder coating.
Performance must be evaluated at the complete coating-system level, using appropriate substrates, preparation methods, film thicknesses and test conditions.
4. Why Texture and Color Consistency Matter
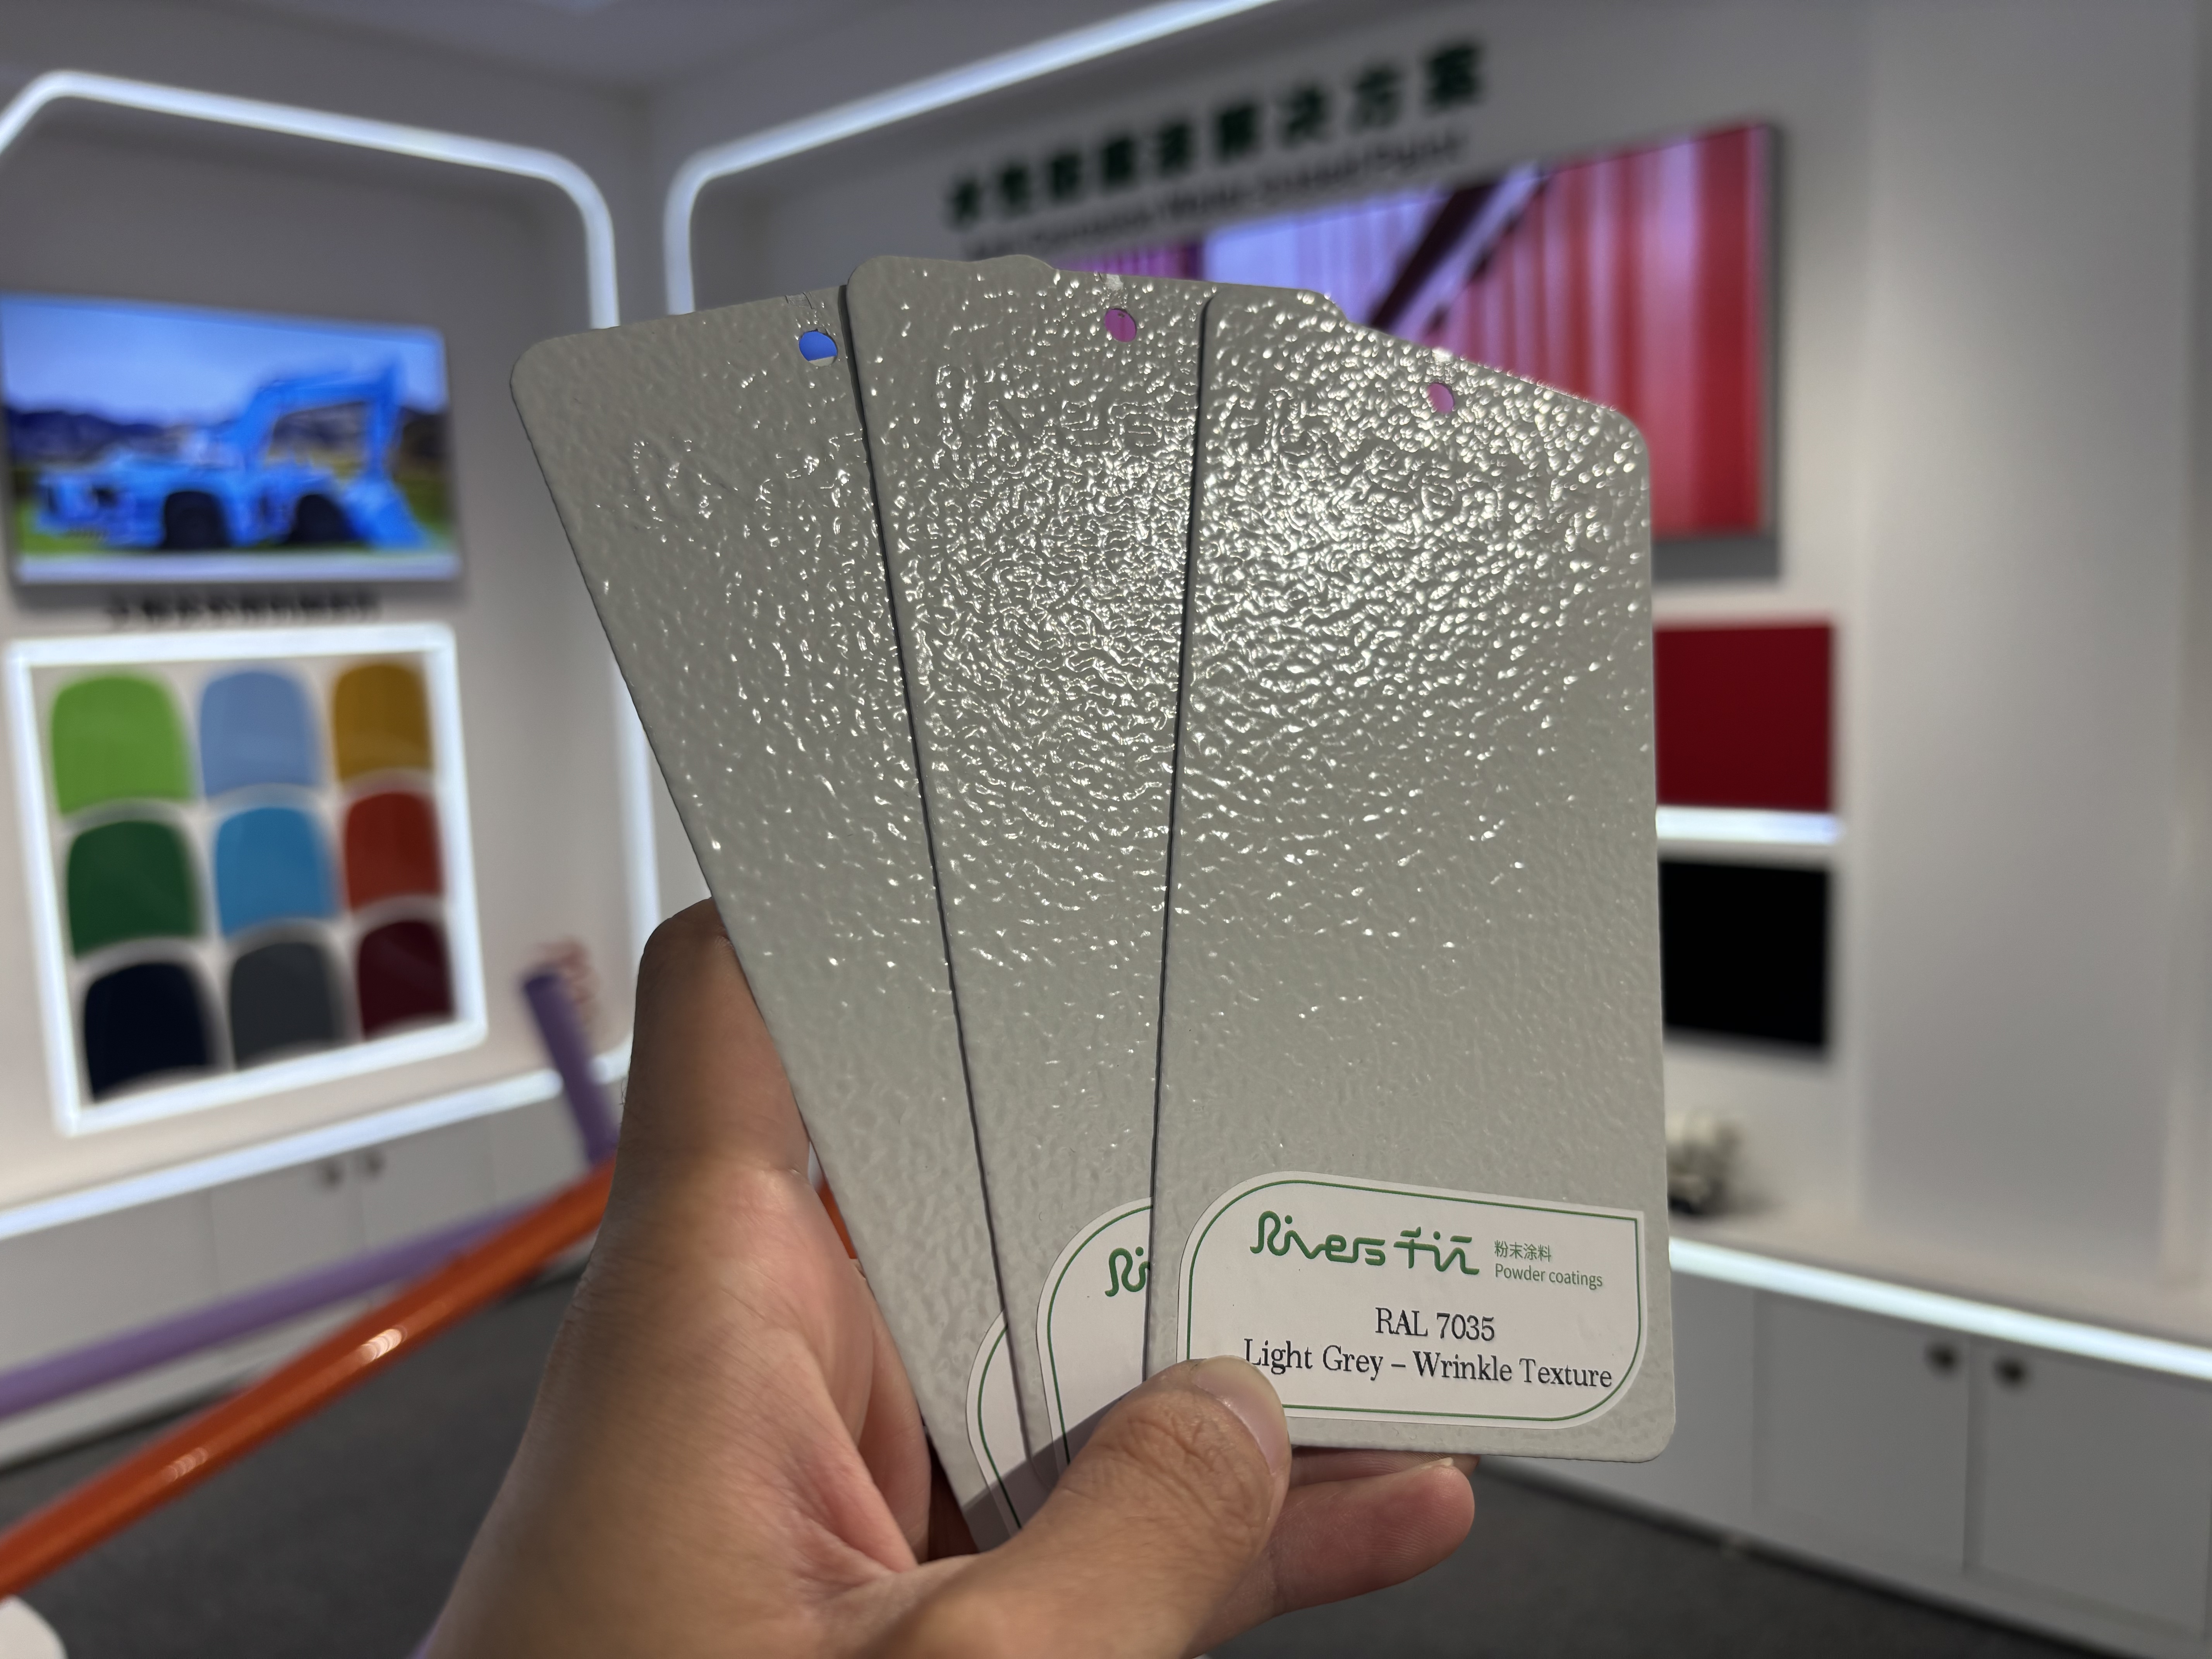
Electrical equipment manufacturers often prefer textured finishes because they provide a professional industrial appearance.
Fine wrinkle and other textured coatings can also reduce the visibility of minor surface imperfections compared with certain smooth finishes.
However, texture development requires careful control.
Film thickness, curing conditions and application parameters can influence the final appearance.
For manufacturers producing thousands of electrical cabinets, even small differences in texture or gloss may become noticeable when components are installed together.
Color consistency is equally important.
A manufacturer producing several cabinet models in RAL 7035 may require the same visual appearance across different production batches.
This is why approved physical samples, agreed appearance tolerances and controlled production conditions are essential.
5. Functional Requirements Must Be Verified Separately
Electrical equipment sometimes requires coatings with additional functional properties.
These may include electrical insulation, flame-retardant behavior or other application-specific performance characteristics.
Such requirements should never be assumed from the coating's appearance or general product category.
For example, UL-related product recognition and UL 94 V-0 flammability classifications address particular requirements within defined scopes. They do not automatically demonstrate that a coating provides the electrical insulation or corrosion resistance needed for a specific enclosure.
Manufacturers should therefore confirm the applicable test method, substrate, coating thickness and product identification before approving a functional powder coating.
Clear technical documentation helps prevent misunderstandings during supplier qualification.
6. Rivers: Industrial Powder Coating Experience for Power Equipment
For electrical equipment manufacturers, choosing a powder coating supplier involves more than comparing product prices.
The supplier must understand industrial production, support consistent surface finishes and provide coating systems appropriate for the operating environment.
Rivers Powder Coatings, a Chinese coating brand established in 1996, has accumulated application experience across power equipment, industrial machinery, architectural metal and other manufacturing sectors.
Within the electrical equipment industry, Rivers has experience with powder coating applications for distribution cabinets, EV charging equipment and energy storage enclosures.
These applications demonstrate the importance of combining decorative appearance with practical industrial protection.
RAL 7035 and RAL 7032 Wrinkle Texture Solutions
Rivers has developed wrinkle-textured powder coating solutions in commonly specified electrical equipment colors, including RAL 7035 and RAL 7032.
These finishes are relevant to electrical cabinets, charging equipment and related metal enclosures.
Depending on the selected formulation, customers can evaluate appearance, weatherability and corrosion-protection requirements together.
For overseas equipment manufacturers, this creates an opportunity to develop coordinated finishes across multiple product models.
Corrosion Protection for Steel Equipment
Rivers has experience developing powder coating systems for steel substrates and projects involving ISO 12944 C3/C4-related corrosion-protection requirements.
For applications requiring additional protection, Rivers can evaluate epoxy primer and suitable weather-resistant topcoat combinations.
The appropriate system must be confirmed through project-specific testing and application assessment.
This system-oriented approach helps customers avoid relying on a single product claim when the actual requirement concerns the complete protective coating.
7. Customized Development and International Technical Support
Electrical equipment manufacturers frequently require customized colors, textures and performance specifications.
A new cabinet design may require a finer wrinkle texture. An overseas charging-equipment manufacturer may need a specific grey shade, gloss level or exterior durability requirement.
Rivers operates 100 dedicated sample-development lines, supporting customized color and finish development across its powder coating portfolio.
For customers, this provides additional resources for comparing alternative finishes and preparing physical samples before production approval.
Rivers also has experience with selected functional powder coating products involving UL-related requirements and UL 94 V-0 testing.
Such qualifications apply only to the relevant products and documented test scopes.
For international projects, Rivers can provide English Technical Data Sheets, Safety Data Sheets and available product-specific test information.
These resources help overseas purchasing, engineering and quality teams evaluate proposed coating systems more efficiently.
8. Why Global Power Equipment Manufacturers Can Consider Rivers
Rivers combines several capabilities relevant to electrical equipment manufacturers:
Industrial application experience: Powder coating experience covering electrical cabinets, charging equipment, energy storage enclosures and other industrial metal components.
Application-oriented corrosion protection: Product development experience involving steel substrates and C3/C4-related protective coating requirements.
Customized surface development: Dedicated sampling resources for industrial colors, wrinkle textures and other finishes.
Technical qualification support: English documentation and available product-specific testing information for international customers.
Together, these capabilities support a practical development process—from initial coating selection and sample approval to actual-line trials and repeat commercial supply.
For equipment manufacturers, the objective is not simply to purchase a powder coating.
It is to establish a reliable surface-finishing solution that supports product quality, manufacturing consistency and long-term supplier cooperation.
9. Conclusion
As electrical infrastructure and energy storage applications continue to develop, surface protection remains an important part of equipment reliability.
The right powder coating system must balance appearance, corrosion protection, application efficiency and relevant functional requirements.
Rivers supports electrical equipment manufacturers with industrial coating experience, customized product development and technical documentation for overseas projects.
Reliable equipment deserves a coating system designed for its real operating environment.
Call to Action
Looking for a reliable powder coating supplier for power equipment or energy storage enclosures?
Contact Rivers with your substrate, target color, installation environment and performance requirements.
Our team can support product selection, customized sampling, corrosion-protection system evaluation and English technical documentation.
Rivers Powder Coatings — Industrial Surface Protection, Built Around Your Application.

Rivers (Qianjiang) Group
Zhaoqing Qianjiang High-Tech Materials Technology Corporation
Guangdong Huajiang Powder Technology Co., Ltd.
Shandong Qianjiang Powder Technology Co., Ltd.
Guangdong Wesdon Rivers Powder Paints Scientifc Research Co., Ltd.
Zhaoqing Qianjiang Coating Co., Ltd.
Zhuhai Zhengdong Chemicals Co., Ltd.
Zhongshan Yonghan Industrial Additives Co., Ltd.
Guangdong Honglang Technology Co., Ltd.
WhatsApp:+86 150 1171 7323
Mail:global@riversqj.com
Address:
Guangdong Huajiang Powder Technology Co., Ltd.
No. 27 Jianshe Road, Dawang High tech Zone, Zhaoqing, Guangdong Province


