
Rivers Insulation & Flame-Retardant Powder Coatings for Power Batteries and Energy Storage
For power battery and energy storage manufacturers, electrical safety, thermal stability and long-term durability are critical to product performance. Rivers provides specialized insulation and flame-retardant powder coating solutions designed for key battery components and energy storage enclosures.

Comprehensive Protection for Power Battery Components
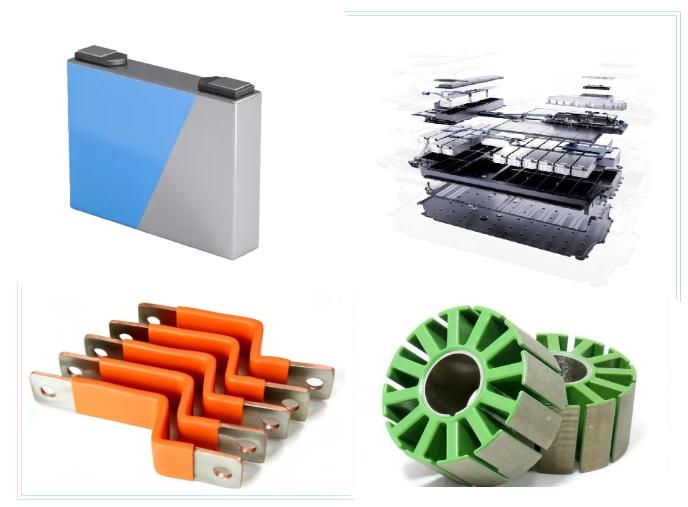
Rivers insulating powder coatings are engineered for a wide range of battery components, including aluminum housings, liquid-cooling plates, copper and aluminum busbars, and magnetic rings.
Aluminum Housings & Side Panels
Designed to work with chromium-free passivation pretreatment, the coating provides reliable electrical insulation and environmental resistance. At a thickness of 120–250 μm, it withstands voltages above 3,800 V and passes 1,000-hour 85°C/85% RH testing. It also offers resistance to temperature changes, heat, antifreeze, lubricating oil and brake fluid, with UL 94 V-0 flame-retardant performance.
Liquid-Cooling Plates
Our liquid-cooling plate coating combines electrical insulation with resistance to heat, temperature cycling, coolant and electrolyte exposure, helping maintain stable protection while supporting efficient thermal management.
Copper & Aluminum Busbars
Designed for high-voltage insulation applications, the busbar coating provides over 30% edge coverage at coating thicknesses of 500–2,000 μm. It also passes 85°C/85% RH testing and delivers resistance to heat and temperature cycling, with UL 94 V-0 flame-retardant performance.
Magnetic Ring Insulation
Specially formulated for magnetic components, the coating withstands AC 1–3 kV without breakdown and maintains performance after 1,000 hours at 125°C, with additional thermal-shock resistance for demanding operating conditions.
Reliable Protection for Energy Storage Enclosures
For energy storage cabinets and enclosures, Rivers provides a combined solution for electrical insulation and corrosion protection.
With a typical coating thickness of 250 ± 50 μm, the system achieves a withstand voltage of DC 4,000–5,000 V for 60 seconds, with leakage current below 1 mA. Insulation resistance exceeds 500 MΩ at DC 1,000 V, while adhesion reaches Grade 0, providing a durable protective barrier for demanding energy storage applications.
Tested for Real-World Performance
Rivers solutions are evaluated across key performance indicators, including:
Dielectric strength and insulation resistance
High-temperature aging
Thermal shock resistance
Corrosion resistance
Adhesion and mechanical performance
Flame-retardant performance
This comprehensive testing approach helps ensure consistent performance from laboratory validation through mass production.

Proven Manufacturing Capability
Rivers is a qualified supplier for LG Electronics Tianjin Appliances Co., Ltd., supporting stable mass production for LG home appliance products. This experience demonstrates our ability to meet the quality, consistency and production requirements of international manufacturing customers.

Your Partner for Safer, More Reliable Energy Equipment
From individual battery components to complete energy storage enclosures, Rivers provides application-specific insulation, flame-retardant and anti-corrosion powder coating solutions backed by technical support and production expertise.
Looking for a coating solution for your battery or energy storage application? Contact Rivers for sample testing, technical consultation and application-specific recommendations.

Rivers (Qianjiang) Group
Zhaoqing Qianjiang High-Tech Materials Technology Corporation
Guangdong Huajiang Powder Technology Co., Ltd.
Shandong Qianjiang Powder Technology Co., Ltd.
Guangdong Wesdon Rivers Powder Paints Scientifc Research Co., Ltd.
Zhaoqing Qianjiang Coating Co., Ltd.
Zhuhai Zhengdong Chemicals Co., Ltd.
Zhongshan Yonghan Industrial Additives Co., Ltd.
Guangdong Honglang Technology Co., Ltd.
WhatsApp:+86 150 1171 7323
Mail:global@riversqj.com
Address:
Guangdong Huajiang Powder Technology Co., Ltd.
No. 27 Jianshe Road, Dawang High tech Zone, Zhaoqing, Guangdong Province


